Simple sensor
May be enough for a visible presence or basic count question with controlled presentation.
addaScan is a Johannesburg-based machine vision integrator that designs vision inspection stations and supplies industrial code readers for factories in Uganda; where site work is agreed, its engineers travel from Johannesburg, and quotes are in US dollars. Scope vision inspection for beverage packaging, printed codes and bag or carton counts on Ugandan production lines. A useful station must connect the observed product, the decision and the physical action. addaScan evaluates triggers, tracking and recovery alongside the camera so a readable mark does not become an unverified claim that a product was removed.
Updated 2 November 2026 · Technical contact: Frank Guo
A conveyor stops with several products between the camera and the reject. Restarting the motor does not necessarily restore which item should be rejected. The controller and inspection software need an agreed recovery rule for that in-process material. An operator should not clear the fault by reusing the last good read or resetting the count while suspect products remain on the line.
Have samples, photos or a line drawing? Start the assessment now, or send them on WhatsApp.
Request a Vision AssessmentWhatsApp +27 68 925 2696Define the evidence and the failure response before selecting a camera, then test each choice on your own products and line conditions.
| Task | Reference and camera view | Exception and boundary |
|---|---|---|
| Bottle label or cap identity | Compare visible product features with the current job and associate the result with the bottle trigger. | Keep a mismatch tied to the physical product until removal is confirmed. |
| Printed codes and marks | Read the required fields under actual contrast, orientation and line-speed conditions. | Unreadable is a separate state; an optical read does not establish tax-mark authenticity or activation. |
| Bag or case counting | Define the count point and track each unit through close spacing, stops and restarts. | Avoid duplicate events and reconcile physical stock within the station before resuming. |
| Pallet handover | Match the pallet label and agreed dispatch fields to the expected order. | Missing order data or an unread label needs a controlled exception, not an assumed match. |
Related solutions: Presence, absence & counting · Cement bag inspection · Bottled water line inspection
Separate, touching, overlapping and stopped bags each need a rule before a count can be trusted at dispatch.
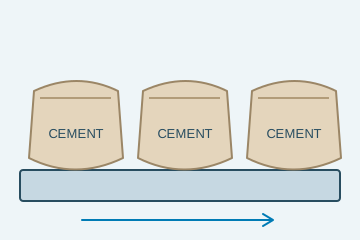
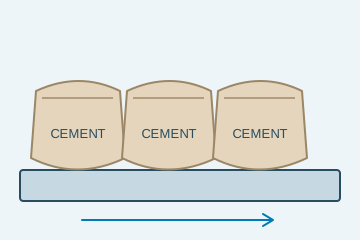
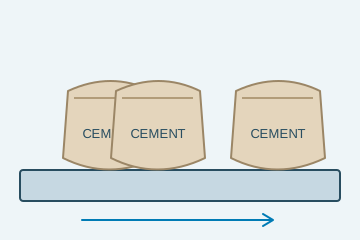
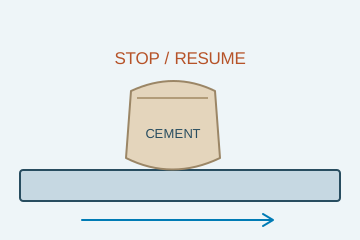
Original schematics from addaScan’s cement-bag counting guide, not photographs from Uganda. Cement bag counting on a dispatch conveyor
Digital or excise-marking requirements should be supplied as a current approved specification. Checking the presence, position or readability of a visible mark is separate from its issue, activation and reporting to a tax platform.
When a Ugandan line stops and restarts, the reader result must still belong to the bag, bottle or carton in front of it. Plan the trigger and tracking with the reader, not afterwards. Grain and feed bags often need a code read on a flexible surface, while beverage cases need a fast read at the case packer.
| Series | Where it fits in this country’s tasks |
|---|---|
| ID3000 | Case and carton codes at the case packer or palletiser infeed. |
| ID5000 | Bag codes whose position shifts with filling and folding. |
| IDH2000 / IDH3000 | Re-checking held packs after a stop, with the operator presenting each pack. |
Series positioning, protection and interfaces as published in the HIKROBOT 2025 Q4 catalogue; the quotation confirms the exact model. No official HIKROBOT partnership or distributor status is claimed. HIKROBOT code reader selection
Industrial Barcode Scanners in Kenya · Request a reader quotation →
Create one event for the physical product.
Track the result to the reject or handover and confirm the outcome.
Reconcile in-process items, references and count events after a stop.
| Scope decision | Information and owner to confirm |
|---|---|
| Restart authority | Agree who reconciles products remaining between the camera and reject after a stop, and who authorises return to normal release. |
| Count and reject records | Define completed count events and confirmed rejects separately. Supply conveyor zones, accumulation behaviour and PLC messages for the project assessment. |
Reader supply, a configured reading point and an integrated station are quoted as different scopes. Freight, import and customs responsibilities, engineering travel, installation, training and support are itemised in USD. How a cross-border quotation is structured
Product standards and certification marks in Uganda sit with the bodies below.
National standards body; product certification and quality marks.
A camera station can check that a required mark or printed field is present and legible on each pack; whether your product needs it is confirmed with the authority or your certification adviser.
Site work is quoted to the factory’s actual location, for example in Kampala, Namanve or Jinja.
Comparing industrial automation companies in Uganda? addaScan’s part is the inspection: it designs vision inspection stations and supplies industrial code readers, and connects them to the PLC, conveyor and reject device that your plant’s automation team, machine builder or local integrator maintains.
Provide product dimensions, spacing, speed, trigger and encoder signals, reject position and confirmation sensor details. Describe planned stops, emergency recovery and how shift counts are reconciled.
Photos, drawings and samples are arranged after initial contact.
Request a Vision Assessment →Compare the relevant method and its limits in these application guides.
Describe the product, the required decision and the factory country. We will use those details to scope the next assessment.