addaScan home
Assessment
Application // 01

Label inspection system for production lines

Label presence, position, label verification and print quality inspection for bottles, jars, cans, cartons and flexible packaging on South African packaging lines.

Technical review: Frank GuoReviewed

Request an assessment for this application
// Short answer

A label inspection system is a camera station on the line that checks every unit: the label is present and straight, it belongs to the product being run, and the printed text is complete. It works when the label is visible from a fixed position and lighting is controlled. It cannot see labels hidden by shrink-film folds or confirm adhesive strength. We prove what it can catch on your own samples before quoting.

// What it checks

What a label inspection system checks

Four checks cover most label faults and print inspection tasks on a bottle, jar or carton line. Which ones you need, and how tight the limits are, is set during the sample test.

01 // Position

Label presence & position

Missing, crooked, shifted or doubled labels, checked against a reference position taught from good samples.

NeedsLabel visible from a fixed camera position
02 // SKU

Wrong label and label mix-up

Label verification against the product selected for the run: the station reads the label barcode, or matches printed text and artwork, so a label mix-up at changeover is caught on the first wrong unit.

NeedsSKU list from the recipe or the line PLC
03 // Print

Print quality inspection

Missing or broken print, smears, misprints and incomplete text in defined areas of the label, including the mandatory text blocks.

NeedsDefect larger than a few pixels at the chosen resolution
04 // Wrap-around

Wrap-around labels

Seam position, overlap and lifted edges on round containers and other cylindrical products, the usual difficulty in bottle label inspection.

NeedsControlled orientation or several camera views
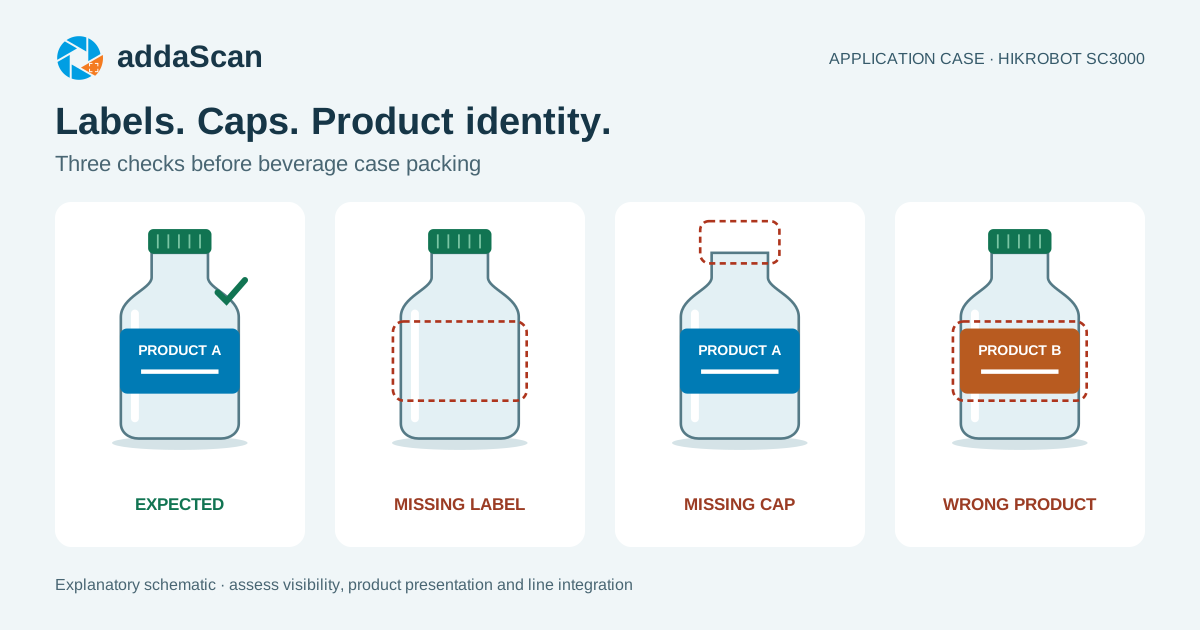
Schematic: expected bottle, missing label, missing cap and wrong product
Application guide · HIKROBOT SC3000

Labels, caps and product mix before packing

A beverage packaging application combines label presence, cap presence and product identity before case packing. See how those decisions differ and when they can share a camera view.

See the beverage inspection application →
// In your words

What operators report: wrong label, missing label, mix-up at changeover

Faults are usually reported by what went wrong, not by the name of an inspection. This is how the common reports map to what a label inspection camera checks.

Label faults as reported on the line, what a label inspection system checks, and its limits
What the line reportsWhat a station checksWhere it stops
“Wrong label on the wrong flavour”, “correct label on the wrong product”Label verification: the label barcode, text or artwork is matched to the SKU selected for the run; a mismatch is rejected or stops the line.If the label is right but the product inside is wrong, the label check cannot see it; that needs a check on the product or container.
“Missing labels”, “upside-down or inverted labels”Missing label detection: label presence, position and orientation against a reference taught from good samples.The label must face a camera; round containers that arrive at any angle need orientation or several views.
“A camera on the labelling machine that stops the line on a wrong label”A camera after the labeller reads each label and compares it with the running SKU; a wrong or missing label rejects the unit or stops the line through the PLC.Whether the line stops or only rejects is agreed in the design; stopping the labeller needs a signal the labeller accepts.
“Crooked, wrinkled or flagged labels”Skew, shift and visibly lifted edges, with the tolerance agreed at the sample test.Adhesion strength is not visible; a label that looks flat but peels later is not detected.
“Label mix-up at changeover – the labels look the same”Every unit is checked from the first one after the changeover, not only a first-off sample; the recipe is selected by the PLC.The station checks against the recipe it is given, so recipe selection must be controlled.
“Smears, misprints, missing information on the label”Print quality inspection in defined areas: missing or broken text, smears and incomplete blocks.Whether the approved artwork is legally correct is an artwork approval task, not a camera task.
“Allergen statement missing from the label”The expected allergen text for the running SKU is verified (OCV) against the approved text.The station does not decide which allergens should be declared.
“Label check every 30 minutes and at every reel change”Continuous checking of every unit, with counts and images kept per batch, which supports label reconciliation records.It supports, but does not replace, the site’s own label control procedure, including what to do if the station fails.
// Limits

Where label inspection stops

We set these boundaries before a project starts, so nobody expects the camera to do what it physically cannot.

Not detectable with a camera

  • Adhesive strength. A camera sees position and appearance, not how well the label is stuck.
  • Hidden print. Text or artwork covered by an opaque sleeve or folded shrink film cannot be inspected.
  • Freely rotating containers with one camera. A single view cannot see a label on a bottle that arrives at any angle; this needs orientation or several cameras.

Works reliably when

  • Lighting is controlled. The station's own lighting, shielded from daylight, keeps images consistent across shifts.
  • Products arrive consistently. Stable spacing and presentation, with a trigger sensor, and an encoder where speed varies.
  • Defects are defined. An agreed list of faults and reference samples, so limits are set on evidence.
// Evidence

What you can check before you ask us

How feasibility is decided on your own samples, and the published budgets of complete line solutions that use this check.

Engineering method

How a sample test is judged

Samples
Good samples that show normal variation, and defective samples for each defect you need to catch, including borderline ones.
Imaging
Imaged under candidate lighting and optics; what is, and is not, visible is recorded.
Acceptance
False rejects and missed defects are agreed in writing and measured at FAT and SAT.
Outcome
A written feasibility conclusion with example images, before any proposal.

The method used on every project; not a measured result.

How to prepare inspection samples →
Budget model

Installed budgets of line solutions that use this check

Staple food bags
R 110 000 – R 770 000
Pipe and cable print
R 110 000 – R 650 000
Meat tray labels
R 160 000 – R 740 000
Basis
Indicative budget for a typical application, in rand, excluding VAT, as at 2 October 2026, low to high configuration. A firm price follows the sample test.

Each figure is for a complete station on that line, not a price for this check on its own.

All line solutions with budgets →
// South Africa

South African labelling rules a label inspection system supports

What R146, the food safety schemes and the recall record say about labels on the line.

The rules set requirements for the label, not for inspection equipment; none of the documents below requires a camera. A label inspection system is one way to confirm, on every unit, that the label the rules require is on the pack, belongs to the product and can be read.

  • R146, regulation 7(2): labels on pre-packaged foodstuffs must be applied so they cannot be separated from the container at the point of sale (R146 gazette copy). Presence and position checks catch missing and visibly loose labels; adhesion itself needs another test.
  • R146, regulation 7(1)(b): the required information must be clearly visible, easily legible and indelible (R146 gazette copy). Print quality inspection covers the mandatory text areas.
  • R146, regulation 43: common allergens are declared in brackets after the ingredient or in a “Contains:” statement (R146 gazette copy). The station can verify that the expected allergen text is printed for the product being run.
  • Draft R3337 (April 2023, not in force): proposes allergens in bold (draft R3337). If it is finalised, whole ranges of artwork change at once, which is exactly when old and new labels get mixed up on the line.
  • FSSC 22000 version 6, 2.5.9(c): line start-up and changeover controls (line clearance) must ensure that labels and packaging from the previous run have been removed from the line (FSSC 22000 Version 6).
  • BRCGS guidance on online verification (Issue 8 FAQ, clause 6.2.4): a site that uses online label verification should challenge it with incorrect packs and test the detection, the reject or line stop and the no-read alarm (BRCGS Issue 8 FAQ). How we build that test into a station is described in the PLC and reject guide.

A consumer product recall South African suppliers carry out is notified to the National Consumer Commission, and its published recall notices include a case in which a food product was packed into the packaging of a different variant and its allergens were therefore not declared (NCC media statement). That is the fault a wrong-label check is designed to stop.
// Station layout

How a label inspection station is laid out

Plan view of a typical single-sided station. The real layout is designed around your line after the site survey.

[Schematic]PLAN VIEW · NOT TO SCALE

Swipe sideways to see the whole station →

Plan view of a label inspection station Products move along a conveyor past a trigger sensor, then under a camera with an angled bar light, and a reject air jet removes failed products further down. An encoder on the conveyor keeps timing correct when speed changes. PRODUCT FLOW → [1] TRIGGER SENSOR [2] CAMERA + LENS [3] BAR LIGHT [4] REJECT (AIR JET) [5] ENCODER
[1] Trigger sensor: tells the station a product has arrived.
[2] Camera: images the label area; resolution is chosen from the smallest defect.
[3] Lighting: angle chosen to avoid glare on glossy labels.
[4] Reject: removes failed products; the PLC tracks each one to this point.
[5] Encoder: keeps reject timing correct when belt speed changes.
// Pass and reject[Illustrative examples]

What a pass and a reject look like

Illustrations of the three most common outcomes. Limits such as how much tilt is acceptable are agreed with you during the sample test.

EXAMPLE // PET BOTTLE

Label correct

Label present, straight within the agreed limit, print complete, and the barcode matches the product selected for the run.

POSITION: IN LIMITCODE: MATCH
EXAMPLE // PET BOTTLE

Label crooked

The label is rotated beyond the limit agreed at the sample test. The product is tracked to the reject point and removed.

POSITION: ✗ OUT OF LIMITACTION: REJECT
EXAMPLE // CARTON

Wrong product label

The code read from the label belongs to SKU B, but the line is running SKU A. This is the typical fault after a changeover.

RESULT: ✗ WRONG SKUACTION: REJECT / ALARM
// Line interface

What we need to know about your line

These conditions decide the station design. None of them has a fixed answer; each is confirmed on site or during the sample test.

Line conditions for a label inspection station
ConditionWhat we need to knowWhy it mattersConfirmed during
Line speedUnits per minute or per hour, and whether the speed varies.Sets exposure time, lighting power and the trigger method. Variable speed usually needs an encoder.Site survey
Product spacingGap between products and how stable it is.Each product must be imaged and rejected on its own; touching products need spacing or a different reject.Site survey
PLC and controlsPLC make and model, spare I/O or network ports.Decides how pass/fail, reject timing and SKU selection are exchanged with the line.Design review
Reject mechanismExisting reject or not; compressed air available.Failed products must leave the line reliably; a confirmation sensor proves they did.Site survey
ChangeoverNumber of SKUs and how the running product is selected.Each SKU needs a recipe; automatic selection from the PLC avoids operator error.Sample test
// Acceptance

How the station is accepted

Two numbers matter, and they pull against each other. We define both, and how they are measured, before FAT and SAT.

01

False reject rate

The share of good products the station rejects. Measured on an agreed set of good samples at line speed; the acceptable level is agreed per project. See reducing false rejects for causes and fixes.

02

Missed defect rate

The share of defective products that pass. Measured with defect samples fed at known positions; for critical faults such as a wrong SKU, the target is set with you.

03

Reference samples & recipe control

Reference samples and recipe settings are documented and access-controlled, so limits do not drift after handover.

// Before we start

What to prepare for the sample test

Before we propose a station, we check your labels on real samples. This is what we ask for; we confirm quantities and shipping with you first.

Sample preparation guide

Good samples

Products that pass today, covering the normal variation: print runs, colours, gloss and matte finishes.

Defective samples

Each fault you need to catch, including borderline cases: crooked, missing, wrong or badly printed labels.

Product information

Container and label drawings or photos, and the list of SKUs that run on the line.

Line information

Line speed, product spacing, PLC make and model, and whether a reject mechanism is fitted.

// FAQ

Label inspection questions

How does the station handle glossy or metallic foil labels?
Glare is the usual problem. Lighting angle, diffuse or dome lighting and polarising filters are used to suppress reflections. Which combination works is confirmed on your own labels during the sample test.
What happens at a product changeover?
Each product has a recipe with its reference label, limits and expected code. The line PLC can select the recipe automatically when the product changes, or the operator selects it on the HMI. Automatic selection avoids running with the wrong recipe.
Can the same camera read the date code as well as the label?
Often, if both are visible to the camera at a suitable resolution. Label checks and code reading (OCR/OCV) can run on the same image; otherwise a second camera is added. Code verification is covered on the OCR/OCV & code inspection page.
Does a label inspection prove the label is stuck on properly?
No. A camera sees position and appearance, not adhesion. A lifted edge that is visible can be flagged, but adhesive strength has to be tested another way.
Is a label inspection machine different from a label inspection system?
Suppliers use both names for the same job. A label inspection machine usually means a standalone unit with its own conveyor section; a label inspection system or station is usually fitted to your existing line; where the main task is print, it is often called a print inspection system. Camera-based units are also sold as a label vision system, and ranges of label vision inspection systems or print inspection systems cover both. Which one suits you depends on space, line speed and whether the reject can be fitted to the current conveyor.
Do you supply a label inspection system for packaging line retrofits in South Africa?
Yes. addaScan, in Johannesburg, designs and commissions label inspection stations for existing packaging lines in South Africa. The station is fitted after your labeller, proven on your own labels first, and connected to your PLC and reject. Indicative budgets are in the cost guide and on the line solution pages.
What is a label verification system?
The part of label inspection that checks each unit carries the right label for the product being run. It compares the label content, such as the barcode, key text or the whole label against a reference image, with the recipe for the product. Label verification is what stops mix-ups at a changeover.
Is one label inspection camera enough, or do I need a full system?
One label inspection camera, usually a smart camera, is often enough when a single label face is checked for presence, position and a code. Several label faces, round containers or many products need a multi-camera system with a controller and a recipe per product.
Can a label camera check the allergen text?
It can confirm that the expected allergen text for the product being run is printed and readable, by verifying it (OCV) against the approved text. It cannot decide which allergens should be declared; that belongs to artwork approval and the allergen control plan.
What causes a product recall involving labels?
Wrong or missing information on the pack is one cause: undeclared allergens, a product packed into the wrong packaging, missing or illegible date and batch codes. Many recalls have other causes, such as contamination, that a label camera cannot see. In South Africa, consumer product recalls are administered by the National Consumer Commission.
// Label inspection

Request an assessment for this application

Describe your labels and your line, and send a few good and bad samples. We will tell you what a station can check and what it would involve.

Use the country guidance to prepare the line data, interfaces and delivery scope for a project assessed from Johannesburg.

NAFDAC label, date and batch checks

Nigerian food labels checked against the artwork submitted for registration.

FDA Ghana label and date-code checks

Approved artwork, manufacture dates and batch codes on Ghanaian packing lines.

Étiquetage en arabe en Algérie

Version, dates et lots sur la ligne ; guide en français.